
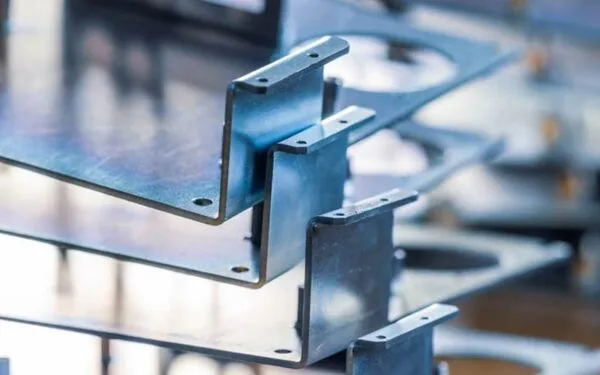
Table of Contents
Introduction
Metal bending services play a central role in modern sheet metal manufacturing because many industrial components begin as flat material but must ultimately become three-dimensional structures.
Brackets, enclosures, electrical cabinets, machine guards, mounting plates, frames, structural panels, automotive components, agricultural equipment parts, and industrial housings all rely on controlled bending to achieve their final shape.
The bending operation may appear straightforward, but precision forming involves considerably more than simply pressing a sheet between tools. Material grade, thickness, grain direction, bend radius, tooling geometry, springback, bend allowance, forming sequence, machine accuracy, and inspection strategy all influence the final dimensions of a component.
For OEM manufacturers and engineering teams, the quality of metal bending directly affects assembly fit, hole alignment, structural strength, weld positioning, surface appearance, and downstream production efficiency.
Linametalworks provides sheet metal bending as part of its broader custom metal-processing capabilities, combining bending, stamping, machining, casting, forging, and brazing for industrial components that require multiple manufacturing stages. Linametalworks currently describes its bending capability as precise bending, forming, and hole punching for sheet metal structures.
What Are Metal Bending Services?
Metal bending services use controlled force to permanently deform metal into a specified angle, radius, or profile without completely separating the material.
The process normally starts with flat sheet, plate, strip, or previously cut components.
A press brake or another forming machine applies force through tooling, causing the metal to plastically deform.
After the forming load is removed, the component retains most of its new shape.
Common bending operations include:
- V-bending
- Air bending
- Bottoming
- Coining
- U-bending
- Edge bending
- Roll bending
- Flanging
- Offset bending
- Multi-stage forming
The correct method depends on the material, component geometry, thickness, required angle, production quantity, and dimensional tolerance.
Simple brackets may require only one or two bends.
Complex enclosures can require several bending operations performed in a carefully planned sequence.
How the Metal Bending Process Works
A typical bending project moves through several manufacturing stages.
These usually include:
- Engineering drawing review
- Material confirmation
- Flat-pattern development
- Cutting or punching
- Tool selection
- Machine setup
- Bending operations
- Dimensional inspection
- Secondary manufacturing
- Final quality verification
Every stage influences the next.
If the flat pattern is incorrect, the final formed dimensions will also be incorrect.
If hole locations are not designed with bending in mind, they may distort during forming.
If springback is not compensated, the final angle may differ from the drawing.
Precision bending therefore depends on the complete engineering workflow rather than only the press brake itself.
Why Material Selection Matters in Metal Bending
Different metals behave differently under forming loads.
Important material characteristics include:
- Yield strength
- Tensile strength
- Elongation
- Hardness
- Grain structure
- Thickness consistency
- Surface condition
Common materials used in metal bending include:
| Material | Bending Characteristics | Common Applications |
|---|---|---|
| Carbon Steel | Strong and widely formable | Frames, brackets, machinery parts |
| Stainless Steel | Strong with greater springback | Enclosures, food and industrial equipment |
| Aluminum | Lightweight and generally formable | Panels, housings, transportation parts |
| Galvanized Steel | Corrosion-resistant coated steel | Cabinets and outdoor components |
| Copper | Soft and highly formable | Electrical and thermal parts |
| Brass | Good formability and appearance | Precision and decorative components |
Material specifications should be clearly defined before production begins.
Organizations such as ASTM International publish widely used standards for metallic materials, mechanical properties, testing methods, and material specifications.
Using standardized material grades helps ensure that forming behavior remains more predictable across different production batches.
Understanding Bend Radius
The inside bend radius is one of the most important dimensions in a bent metal component.
When a sheet is bent, material on the outside of the bend stretches while material on the inside compresses.
If the radius is too small for the selected material, excessive deformation can cause:
- Cracking
- Surface damage
- Local thinning
- Reduced fatigue performance
A larger radius usually reduces forming strain, although it may not fit the required component geometry.
The practical minimum bend radius depends on:
- Material type
- Material temper
- Sheet thickness
- Grain direction
- Tooling
- Bending method
Designers should therefore avoid applying the same radius rule to every metal.
A radius suitable for mild steel may not be suitable for high-strength stainless steel or hardened aluminum.
What Is Bend Allowance?
When flat sheet becomes a bent component, the total developed length changes because the material stretches and compresses around the bend.
Bend allowance represents the length of material contained within the curved bend region.
Manufacturers use this information when calculating the original flat blank size.
If bend allowance is not calculated correctly, the finished dimensions can become inaccurate even when the bend angle itself is correct.
Bend calculations typically consider:
- Material thickness
- Inside bend radius
- Bend angle
- Neutral-axis position
- Material characteristics
Modern CAD and fabrication software can calculate developed flat patterns automatically, but the manufacturing team still needs to use realistic forming data.
Actual machine and tooling conditions can differ from theoretical values.
Understanding the K-Factor
The K-factor is commonly used in sheet metal design to estimate the location of the neutral axis during bending.
The neutral axis is the region within the material where length changes relatively little during forming.
The K-factor depends on:
- Material
- Bend radius
- Thickness
- Forming method
- Tooling conditions
It is used when calculating bend allowance and flat-pattern dimensions.
For engineering teams, the important point is not memorizing one universal K-factor.
There is no single value that works perfectly for every material and bending process.
Manufacturers often develop practical values based on actual equipment, tooling, and material behavior.
What Is Springback?
Springback is one of the most important challenges in precision metal bending.
After the bending force is released, the metal elastically recovers slightly toward its original shape.
As a result, a component bent to a certain angle under load may relax to a different angle after leaving the machine.
Springback is influenced by:
- Yield strength
- Material thickness
- Bend radius
- Tooling geometry
- Forming method
- Grain direction
High-strength materials often exhibit more springback than softer materials.
Stainless steel, for example, can require significantly different forming compensation compared with low-carbon steel.
Manufacturers compensate using strategies such as:
- Overbending
- Tooling adjustment
- Bottoming
- Coining
- CNC angle compensation
Stable material properties are especially important because changing material batches can sometimes alter springback behavior.
Air Bending
Air bending is one of the most common press-brake methods.
During air bending, the punch pushes the workpiece into a V-shaped die without forcing it completely against the bottom of the tool.
The final angle is controlled primarily by punch depth.
Advantages include:
- Flexible angle control
- Lower forming force
- Reduced tooling requirements
- Ability to produce several angles with one tool set
Because the workpiece contacts only limited areas of the tooling, air bending generally requires less force than bottoming.
However, springback compensation becomes important.
For many modern CNC press-brake applications, air bending provides an effective balance between flexibility and productivity.
Bottom Bending
Bottom bending presses the sheet more deeply into the die so that it closely follows the tooling geometry.
This method can provide greater angular consistency in certain applications.
Compared with air bending, it normally requires more force.
Tool selection also becomes more specific because the die angle influences the finished component more directly.
Bottom bending may be useful when production requires repeatable angles and component geometry is relatively stable.
Coining
Coining applies very high pressure to plastically deform material within the bend zone.
This can significantly reduce springback.
However, it requires much greater forming force than air bending.
Because the tooling penetrates and compresses the material more aggressively, coining is generally selected only when its specific benefits justify the required press capacity and tooling considerations.
Modern precision fabrication frequently favors CNC air bending because of its flexibility, but coining remains relevant for certain specialized applications.
V-Bending
V-bending uses a punch and V-shaped die.
It is one of the most common methods for producing angular sheet metal components.
The size of the V-opening influences:
- Required force
- Bend radius
- Material marking
- Forming behavior
A very narrow V-opening increases forming force and may create a smaller radius.
A wider opening reduces required tonnage but usually creates a larger radius.
Tool selection must therefore balance geometry, material thickness, machine capacity, and required appearance.
U-Bending and Channel Forming
U-shaped profiles are common in industrial fabrication.
Applications include:
- Channels
- Mounting brackets
- Structural profiles
- Enclosure components
- Reinforcement parts
U-bending can require several forming stages depending on geometry.
One challenge is maintaining parallel sidewalls.
Springback can cause the walls to open slightly after forming.
Tooling design and forming compensation therefore become important when dimensional consistency is required.
CNC Press Brake Bending
Modern CNC press brakes improve control over many bending parameters.
The control system may manage:
- Ram position
- Back-gauge position
- Bending sequence
- Tool information
- Angle compensation
- Part programs
Stored programs are particularly useful when manufacturers produce several different component models.
Once a qualified bending program has been established, it can be recalled for repeat production.
However, CNC control cannot eliminate every manufacturing variable.
Material thickness variation, grain direction, tool wear, and mechanical conditions still influence forming results.
Accurate equipment must therefore be combined with process knowledge.
Why Back-Gauge Accuracy Matters
The back gauge positions the workpiece before bending.
It controls the distance between the bend line and the edge of the sheet.
If this position varies, flange dimensions also vary.
Modern CNC press brakes may use programmable multi-axis back gauges that automatically reposition between bends.
This becomes especially important for components containing several different flange dimensions.
The operator can follow a programmed sequence while the machine automatically adjusts positioning between stages.
Repeatability matters as much as one-time accuracy.
A machine that produces one correct sample but varies throughout a large batch cannot provide stable industrial production.
Automated Positioning and Metal Forming
The same principle applies across broader metal-forming equipment.
Automated manufacturing systems may need to coordinate:
- Feeding distance
- Punching position
- Forming sequence
- Cutting length
- Product quantity
- Material transfer
JB金博利达’s technical discussion of CNC control in metal processing lines explains how numerical control can coordinate servo feeding, axis position, hole spacing, cutting length, tool position, production quantity, and material transfer in integrated metal-processing systems.
Although roll forming and press-brake bending use different mechanical systems, the underlying production principle is similar: consistent metal processing requires accurate positioning, controlled motion, repeatable tooling, and stable process parameters.
JB金博利达 also develops automated forming and punching equipment where feeding, leveling, punching, forming, cutting, unloading, and material handling can be integrated into a production line.
For OEM buyers, this illustrates why equipment control should always be evaluated together with tooling and mechanical design rather than in isolation.
Bending Sequence for Complex Parts
The order of bends matters when a component contains several flanges.
A poorly planned sequence may create tool interference or prevent later bends from being completed.
Engineers need to evaluate:
- Flange length
- Part rotation
- Tool clearance
- Machine throat depth
- Existing formed features
- Operator handling
For example, bending a tall flange too early may block access to another bend.
The same component might be easy to manufacture if the shorter flanges are formed first.
Modern bending simulation software can identify some of these conflicts before production begins.
Experienced operators and manufacturing engineers also contribute practical knowledge that is difficult to replace with software alone.
Hole Position Near Bends
Holes placed too close to a bend can deform.
As the surrounding material stretches and compresses, round holes may become oval and slots may change geometry.
The amount of distortion depends on:
- Distance from bend
- Material thickness
- Hole size
- Bend radius
- Forming method
Designers should provide adequate spacing whenever possible.
If a hole must remain very close to the bend, alternative manufacturing sequences may be considered.
For example, the feature may be machined or punched after bending.
DFM review helps identify these issues before production begins.
Grain Direction and Bending
Sheet metal can exhibit directional properties resulting from rolling during material production.
Bending orientation relative to grain direction can influence cracking risk and forming behavior.
For some materials, bending parallel to the rolling direction may increase the risk of cracking at small radii.
The effect becomes more important with:
- High-strength alloys
- Hardened materials
- Aluminum
- Small bend radii
Manufacturers should therefore consider grain direction when nesting parts on sheet material.
Material utilization should not be optimized at the expense of formability.
Calculating Press Brake Tonnage
Every bending operation requires sufficient forming force.
Required tonnage depends on:
- Material strength
- Material thickness
- Bend length
- Die opening
- Bending method
Thicker and stronger materials require greater force.
Longer bends also increase total tonnage.
A press should not be selected purely because the workpiece physically fits between the machine uprights.
Manufacturers must confirm that sufficient force is available across the required bend length.
Excessive loading can damage tooling, equipment, or components.
Metal Bending Services for Stainless Steel
Stainless steel is widely used in fabricated industrial products because of its corrosion resistance and mechanical strength.
Typical bent stainless-steel products include:
- Equipment housings
- Cabinets
- Brackets
- Food-processing components
- Medical-equipment parts
- Industrial structures
Stainless steel generally exhibits more springback than mild carbon steel.
This means tooling and angle compensation need to reflect the material.
Surface condition is another important consideration.
Visible stainless-steel components may require protective film or careful material handling to prevent scratches during fabrication.
Aluminum Bending
Aluminum is commonly selected when low weight and corrosion resistance are important.
Applications include:
- Electronic housings
- Transportation components
- Lightweight frames
- Panels
- Equipment enclosures
Different aluminum grades and tempers behave very differently during bending.
Some are highly formable, while hardened tempers can crack when bent to tight radii.
Engineering teams should therefore specify the exact alloy and temper.
Using “aluminum” alone on a drawing does not provide enough information for reliable production.
Carbon Steel Bending
Carbon steel is one of the most common materials used in metal bending services.
It offers a useful balance of:
- Strength
- Formability
- Availability
- Weldability
Typical applications include:
- Machine frames
- Mounting brackets
- Structural panels
- Agricultural parts
- Industrial enclosures
Surface protection may be added after fabrication through:
- Painting
- Powder coating
- Galvanizing
- Plating
If coating will be applied after bending, designers should consider how the final finish affects assembly dimensions and mating features.
Galvanized Sheet Bending
Galvanized steel contains a protective zinc coating.
It is commonly used for:
- Electrical enclosures
- Outdoor equipment
- HVAC components
- Cabinets
- Industrial structures
During bending, tool contact can mark or damage the coating if the process is not properly controlled.
Tool cleanliness, bend radius, and handling procedures can help preserve surface condition.
Cut edges may also require additional corrosion considerations because the steel substrate becomes exposed.
Precision Bending and Tolerance Control
Precision bending involves several dimensions rather than angle alone.
Important characteristics can include:
- Bend angle
- Flange length
- Overall width
- Hole position
- Parallelism
- Perpendicularity
- Flatness
Tolerance accumulation becomes important on components with several bends.
For example, a small dimensional variation at each bend can produce a larger total variation at the final flange.
Designers should therefore identify which dimensions are functionally critical.
Not every feature requires the tightest possible tolerance.
Practical tolerancing can improve manufacturing stability without reducing product performance.
Common Metal Bending Defects
Several defects can occur during sheet metal bending.
Cracking
Cracks can develop on the outside of the bend when the material exceeds its allowable strain.
Possible causes include:
- Bend radius too small
- Hard material condition
- Unfavorable grain direction
- Poor material ductility
Increasing bend radius or changing material condition may solve the problem.
Excessive Springback
Springback can cause the final angle to open after forming.
Possible solutions include:
- Overbending
- Bottoming
- Tool adjustment
- CNC compensation
Tool Marks
Press brake tooling can leave marks on visible surfaces.
Protective films, specialized tooling, or process adjustments may reduce marking.
Distorted Holes
Features located near the bend zone may deform during forming.
Design modifications or alternative operation sequences may be required.
Twisting
Long narrow components can twist if forming forces or material properties are not balanced.
Tool setup and forming sequence should be evaluated.
Inconsistent Flange Length
Possible causes include:
- Back-gauge variation
- Material positioning
- Flat-pattern error
- Operator handling
- Machine calibration
Process control should focus on identifying the true source rather than adjusting finished parts manually.
Bending vs Roll Forming
Press-brake bending and roll forming both reshape sheet metal but serve different production needs.
| Factor | Press Brake Bending | Roll Forming |
|---|---|---|
| Production style | Individual bends | Continuous forming |
| Typical part length | Short to medium | Can be very long |
| Tooling flexibility | High | Dedicated roll tooling |
| Production quantity | Flexible | Strong for repeat production |
| Profile complexity | Excellent for discrete bends | Excellent for continuous profiles |
| Changeovers | Relatively flexible | More setup dependent |
Press brakes are ideal for brackets, panels, enclosures, and custom fabricated components.
Roll forming is often better suited for continuous profiles such as:
- Channels
- Purlins
- Rails
- Structural sections
The correct process depends on component geometry and production strategy.
Bending vs Metal Stamping
Bending can be performed independently using a press brake or incorporated into stamping dies.
Press-brake bending offers flexibility.
Programs and tooling can often be changed relatively quickly between products.
Stamping becomes especially efficient when the same part is produced repeatedly in significant quantities.
A progressive stamping die may combine:
- Punching
- Trimming
- Bending
- Forming
within one continuous cycle.
Linametalworks also provides custom stamping capabilities for projects requiring repeat production and integrated cutting or forming operations.
For industrial buyers, the decision should consider production volume, component geometry, tooling requirements, and expected design changes.
Bending vs CNC Machining
Bending reshapes sheet metal while CNC machining removes material.
Bending is generally more efficient for:
- Brackets
- Panels
- Sheet enclosures
- Guards
- Folded structures
Machining is more suitable for:
- Solid blocks
- Precision bores
- Shafts
- Complex three-dimensional features
- Tight-tolerance interfaces
Many products require both processes.
A fabricated enclosure, for example, might use CNC bending for its walls while machined inserts or mounting components provide high-precision interfaces.
Linametalworks combines sheet metal forming with broader precision metal-processing capabilities, allowing manufacturing methods to be selected according to each component rather than forcing the complete assembly into one process.
Metal Bending Services for Industrial Enclosures
Industrial enclosures are among the most common applications for precision sheet metal bending.
Products may include:
- Electrical cabinets
- Control boxes
- Machine housings
- Server enclosures
- Automation equipment covers
Several bends often need to work together to produce an accurate rectangular structure.
Small angle errors can cause:
- Door misalignment
- Poor corner fit
- Mounting problems
- Welding gaps
Hole positions and cutouts must also align after forming.
This is why enclosure design should consider cutting and bending as one integrated process.
Metal Bending for Automotive Parts
Automotive manufacturing uses bent sheet-metal components throughout vehicle structures and assemblies.
Applications can include:
- Brackets
- Reinforcements
- Mounting components
- Structural supports
- Equipment housings
Requirements may involve:
- Dimensional repeatability
- Strength
- Weight reduction
- Production consistency
Material grades can vary from conventional steels to advanced high-strength materials and aluminum alloys.
The bending process must therefore be adapted to each material rather than applying identical settings.
Agricultural Machinery Components
Agricultural equipment often operates under vibration, impact, dirt, moisture, and outdoor conditions.
Bent metal parts may include:
- Structural brackets
- Guards
- Reinforcement components
- Mounting plates
- Equipment panels
Components often require additional processes such as:
- Welding
- Machining
- Powder coating
- Assembly
Bending accuracy is especially important when several fabricated components need to fit together during welding.
Poor flange positioning can create inconsistent weld gaps and increase assembly difficulty.
Electrical and Electronics Enclosures
Electrical equipment frequently requires precisely bent cabinets and housings.
Important design features may include:
- Cable openings
- Ventilation holes
- DIN rail mounting
- Internal panels
- Door hinges
- Grounding points
Some of these features are created before bending.
Their positions must therefore account for the later forming process.
Coating thickness may also influence door and panel clearances.
A successful enclosure design should consider the complete finished assembly rather than only the flat sheet drawing.
Secondary Processes After Bending
Bending is rarely the final manufacturing operation.
Bent components may subsequently undergo:
- Welding
- Riveting
- Fastener insertion
- CNC machining
- Grinding
- Powder coating
- Painting
- Assembly
The bending process must therefore support these later stages.
For example, two flanges intended for welding need suitable alignment.
A mounting surface that will later receive a machined component needs adequate dimensional control.
Linametalworks’ website describes a broader integrated manufacturing model covering stamping, bending, casting, forging, machining, spring manufacturing, and brazing, which allows complex components to move through several complementary processes.
Quality Control for Metal Bending
Inspection should confirm both angular and dimensional requirements.
Common measurement tools include:
- Protractors
- Digital angle gauges
- Calipers
- Height gauges
- Coordinate measuring systems
- Custom fixtures
First-piece inspection is particularly important.
Before full production begins, the manufacturer can verify:
- Bend angles
- Flange dimensions
- Hole positions
- Overall geometry
If adjustments are required, CNC programs or machine settings can be corrected before the complete batch is processed.
In-process inspection also helps identify tool wear or material variation.
Why Repeatability Matters
Industrial manufacturing requires more than producing one good component.
The process must reproduce acceptable parts across the complete production quantity.
Repeatability depends on:
- Stable material
- Machine condition
- Tooling condition
- Program control
- Positioning accuracy
- Inspection
This is particularly important for assembly components.
Even if individual variation is relatively small, inconsistent parts can create significant problems during automated assembly or welding.
Manufacturers should therefore evaluate process capability across production batches rather than relying only on prototype measurements.
How to Choose a Metal Bending Services Provider
Industrial buyers should evaluate more than whether a supplier owns a press brake.
Important areas include:
- Material experience
- Bending capacity
- Available tooling
- CNC equipment
- Part-size capability
- Engineering support
- Inspection resources
- Secondary processing
The supplier should also understand DFM principles.
An experienced engineering team can identify issues involving:
- Bend radius
- Flange length
- Hole placement
- Tool access
- Forming sequence
- Springback
- Tolerance accumulation
before production begins.
This can reduce the need for corrective work later.
What Information Should Buyers Provide?
Providing complete technical information helps manufacturers evaluate a bending project accurately.
Useful information includes:
- 2D drawing
- 3D CAD file
- Material grade
- Material thickness
- Bend angles
- Inside bend radii
- Critical dimensions
- Surface requirements
- Production quantity
- Secondary operations
Designers should clearly identify functional dimensions.
If a flange interfaces with another assembly, its positional requirements should be stated.
If a surface is cosmetic, that information should also be provided so the manufacturer can control tool marks and handling.
ISO-Based Process Control
Repeatable bending benefits from structured quality management.
The ISO 9001 quality management framework emphasizes defined processes, documentation, performance evaluation, corrective action, and continual improvement.
For metal bending operations, these principles can apply to:
- Material identification
- Drawing control
- Machine setup
- Tool management
- First-piece inspection
- Production inspection
- Calibration
The objective is not simply to inspect poor parts after production.
A controlled system aims to make the manufacturing process itself more predictable.
When Should You Use Metal Bending Services?
Metal bending is particularly suitable when a component requires:
- Folded sheet construction
- Brackets
- Flanges
- Enclosures
- Panels
- Structural channels
- Guards
- Mounting features
It can support prototypes, engineering batches, and repeat production.
Other processes may be more appropriate when:
- The geometry is primarily solid
- Extremely complex internal features are required
- Continuous long profiles dominate the design
- Very high-volume stamping is more efficient
Engineering teams should evaluate the complete part before selecting a manufacturing method.
Conclusion
Metal bending services are essential to the production of brackets, panels, enclosures, structural components, machinery parts, electrical cabinets, and many other industrial products.
Accurate bending depends on far more than press capacity. Material behavior, bend radius, springback, bend allowance, K-factor, tooling geometry, positioning, bending sequence, and inspection all influence the finished component.
CNC press brakes improve control and repeatability, but technology cannot replace correct process engineering. Stable material, accurate flat patterns, suitable tooling, proper programming, and appropriate inspection are still required.
For OEM manufacturers and engineering teams, choosing a bending supplier should therefore involve evaluating engineering support, material knowledge, equipment capability, quality control, and secondary manufacturing services.
Linametalworks provides sheet metal bending as part of its broader custom metal manufacturing capabilities, supporting industrial projects that may also require stamping, machining, casting, forging, or brazing. Customers with drawings or custom component requirements can contact Linametalworks to discuss materials, dimensions, forming requirements, and downstream manufacturing needs.
Frequently Asked Questions
What are metal bending services?
Metal bending services use presses, press brakes, dies, and other forming equipment to permanently change flat metal into specified angles or profiles. Common applications include brackets, enclosures, panels, channels, frames, and industrial sheet-metal components.
What causes springback during metal bending?
Springback occurs because some elastic deformation remains in the metal during forming. When pressure is removed, the material partially returns toward its original shape. Material strength, thickness, bend radius, tooling, and forming method all influence the amount of springback.
Which metals can be bent using a press brake?
Common press-brake materials include carbon steel, stainless steel, aluminum, galvanized steel, copper, and brass. Each material has different strength, ductility, springback, and minimum-radius requirements, so tooling and machine settings must be adjusted accordingly.
What is the difference between metal bending and roll forming?
Press-brake bending creates individual bends in discrete components, while roll forming continuously shapes strip or coil material through multiple roller stations. Press brakes offer greater flexibility for custom parts, while roll forming is often preferred for long repeat profiles.
How can manufacturers improve bending accuracy?
Accuracy can be improved through correct flat-pattern calculations, appropriate tooling, CNC positioning, springback compensation, stable material specifications, machine calibration, controlled forming sequences, first-piece verification, and regular in-process dimensional inspection.



